MGW Glass
Choosing between PVB and SGP is not simply a matter of price or brand reputation. It is a performance decision affecting safety, durability, appearance, and installation risk. This guide examines how to identify high-quality PVB vs SGP interlayers through measurable evidence, not attractive product descriptions. The National Glass Association’s Laminated Glass Design Guide emphasizes interlayer selection, glass configuration, and edge conditions as critical factors. ASTM C1172 also establishes performance requirements for laminated architectural flat glass.
PVB is widely used in residential glazing, façades, skylights, and vehicle glass. It offers strong adhesion, sound-control options, and broad processing experience. SGP, commonly described as an ionoplast interlayer, generally provides higher stiffness and better post-breakage support. That difference becomes visible in large panels, structural glazing, and areas exposed to wind or impact. Examine the technical datasheet closely. Check thickness, tensile strength, shear modulus, visible-light transmission, moisture resistance, and certified test results. A clear sample should show minimal haze, clean edges, and consistent bonding after lamination.
This sounds simple.
It is not.
Real performance also depends on glass design, autoclave control, edge sealing, humidity, and installer skill. ASTM E1300 may guide glass thickness selection, but it does not replace project-specific engineering. EN 14449 and relevant local standards provide additional conformity references. One assumption deserves rechecking: a more expensive interlayer is not automatically the better choice. Reliable buyers should request batch certificates, third-party test reports, and production traceability. This article compares China’s leading suppliers while recognizing an uncomfortable truth: marketing claims can look precise, yet weak documentation still creates serious uncertainty.
China Top 10 How to Identify Quality PVB vs SGP?
PVB is a polymer interlayer made from polyvinyl butyral, plasticizers, and stabilizing additives. Its flexible structure supports adhesion, sound reduction, and impact protection in laminated glass. SGP is an ionoplast interlayer with ionic bonding sites and a much stiffer molecular network. It usually transfers loads more efficiently between glass sheets. This difference affects deflection, edge stability, and long-term performance.
Look closely at the interlayer before processing. Quality PVB should appear clear, uniform, and free from visible particles, wrinkles, or trapped air. SGP should show consistent thickness and clean edges, especially after cutting. Do not judge quality by stiffness alone. A soft material is not automatically weak, and a rigid material is not automatically suitable for every project.
In factory inspections, I check thickness records, surface cleanliness, adhesion data, and storage conditions. Moisture exposure can reduce bonding reliability, particularly when handling is careless. It matters. Laboratory tests should examine haze, yellowness, tensile strength, shear behavior, and resistance to heat and humidity. Visual checks remain useful, but they can miss internal defects. I have seen apparently perfect sheets fail after poor storage or incorrect lamination settings. Specifications should therefore match the glass design, climate, edge exposure, and required safety performance.
The index compares representative room-temperature values, with PVB set to 1.0. SGP is an ionoplast interlayer based on partially neutralized ethylene-methacrylic acid, while PVB is a thermoplastic polyvinyl butyral interlayer. Typical SGP stiffness is much higher, while PVB generally provides greater flexibility and elongation. Actual performance varies with formulation, temperature, thickness, moisture, and test method.
When comparing PVB and SGP suppliers in China, verify the factory before judging the interlayer. Request the business license, registered address, export records, and manufacturing scope. The legal entity should match every quotation, certificate, and bank document. Check the registration through China’s official enterprise information system. Do not rely on a polished website.
Ask for current ISO 9001 certification, but inspect its scope and issuing body. A certificate covering trading activities cannot prove production capacity. Request laminated-glass test reports showing glass thickness, interlayer type, dimensions, and testing standards. Confirm the report number directly with the laboratory. Also check issue dates and product descriptions. Small mismatches matter.
UNEP’s 2023 Global Status Report states that buildings consume about 30% of global final energy and produce around 26% of energy-related emissions. This increases the importance of reliable façade and safety-glass documentation.
Require batch numbers, production dates, interlayer thickness records, and storage conditions. For SGP, confirm the specified stiffness and tear-strength data; for PVB, check adhesion, haze, and moisture-control results. I have seen documents with correct logos but missing batch traceability. That is a warning.
My own checklist is not perfect, either. An independent pre-shipment inspection can expose gaps that paperwork hides.
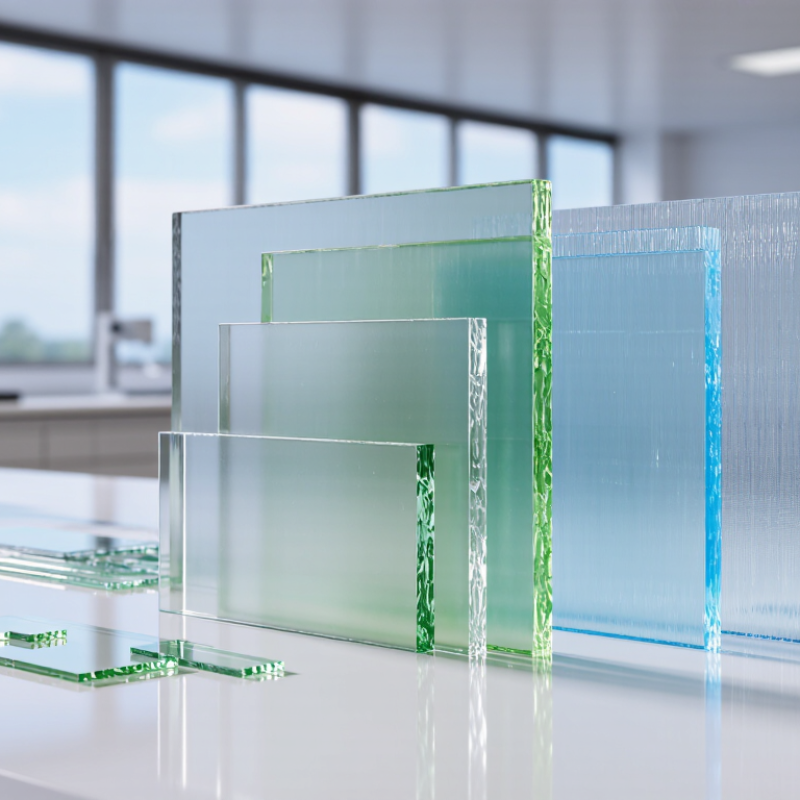
Quality PVB and SGP interlayers require more than a quick visual check. Inspect the film under neutral white light. Clear material should show consistent transparency, without milky areas, bubbles, streaks, or embedded particles. Compare samples against a clean white background. Slight color differences become easier to notice there.
Measure thickness at several points with a calibrated gauge. Readings should stay close to the specified tolerance. Uneven thickness may affect lamination results and optical performance. Check the surface with clean gloves. It should feel smooth, dry, and free from scratches, wrinkles, dents, and dust. Do not judge clarity through plastic packaging alone. Packaging can hide small defects.
Tips: Keep inspection records with photos, batch details, and measurement results. A trained inspector should check both PVB and SGP under identical conditions. Use a haze meter or spectrophotometer when the project demands precise data. Simple visual checks help, but they are not enough. Even experienced inspectors can miss faint distortion or gradual color change. I have found that repeated measurements often reveal small inconsistencies overlooked during the first inspection. Pay attention to storage marks, too. A clean-looking roll may still need further testing before approval.
When comparing China’s top ten PVB and SGP suppliers, examine adhesion before appearance. A clean glass surface matters greatly. In a controlled peel test, the interlayer should resist separation without sudden tearing. PVB usually offers strong adhesion and useful sound reduction. SGP often delivers firmer bonding, but processing conditions remain critical. Do not trust appearance alone. Some suppliers show only fresh samples; aging data is more revealing.
For strength, compare interlayer thickness, glass makeup, and post-breakage behavior. SGP generally provides greater stiffness and better support after glass cracking. PVB can absorb impact energy and remain flexible under movement. Ask for bending tests before and after heat and humidity aging. A small edge chip can change results. This is where my own earlier checks were too optimistic. One impressive load test cannot represent every installation.
Moisture resistance requires more than a dry-room sample. Inspect edge sealing, autoclave records, water immersion results, and storage conditions. Clouding or bubbles near the edge may indicate poor processing or moisture entry. Safety depends on glass retention after breakage, not only on initial strength. When broken, the interlayer should hold fragments together and reduce falling hazards. Request impact, fragmentation, and post-breakage retention reports. Test documents should identify specimen size, temperature, and aging time. If the data is vague, pause. Ask for another sample and inspect its edges carefully.
China Top 10: How to Identify Quality PVB vs SGP?
Quality evaluation should begin with current testing results, not attractive samples. Request reports for tensile strength, elongation, tear resistance, adhesion, haze, yellow index, moisture, and thickness tolerance. Results should identify the exact product grade, test method, laboratory, and testing date. A report without batch information is weak evidence. Compare several production lots, because one excellent sample can hide unstable performance.
Certifications also require careful checking. Confirm the certificate scope, expiry date, issuing body, and relevant production site. ISO 9001 supports process control, while ISO/IEC 17025 accreditation strengthens laboratory credibility. Certifications do not replace product testing. Packaging matters too. Quality interlayers should use sealed moisture-barrier bags, suitable cartons, and clear storage instructions. Check for damaged seals, condensation, unusual odor, or uneven rolls. Small details matter.
Tips: Record the batch number, production date, thickness, and supplier documents before approval. Keep photographs of labels and packaging. Traceability should connect the roll to raw-material records, inspection results, and shipment details. Ask how quickly missing records can be retrieved. If answers remain vague, pause the evaluation. This is not always convenient. It can prevent expensive rework later. A practical review may still miss hidden variation, so repeat testing is wise.
| No. | Evaluation Dimension | Quality PVB Indicators | Quality SGP / Ionoplast Indicators | How to Verify the Result |
|---|---|---|---|---|
| 1 | Material Identification | Polyvinyl butyral interlayer designed for laminated glass. Confirm grade, nominal thickness, color, and intended application. | Ionoplast interlayer with higher stiffness than conventional PVB. Confirm grade, nominal thickness, color, and structural-glazing suitability. | Match the product label, technical data sheet, purchase specification, and certificate of analysis. Do not identify material by appearance alone. |
| 2 | Thickness and Dimensional Tolerance | Thickness should be within the supplier’s declared tolerance, with uniform width and length. Typical commercial thicknesses include approximately 0.38 mm, 0.76 mm, and 1.14 mm, depending on the specification. | Thickness should be within the declared tolerance and suitable for the required structural design. Multiple plies may be required for specific performance levels. | Measure at several points using a calibrated thickness gauge. Compare the average and point-to-point variation with the approved specification, not with an assumed universal tolerance. |
| 3 | Optical Appearance | Clear or specified-color film should be free from excessive haze, streaks, gels, foreign particles, wrinkles, and edge contamination. | The film should show consistent clarity and color with no visible inclusions, surface damage, wrinkles, or abnormal haze. | Inspect under controlled lighting and record haze, visible defects, and color against the approved sample. Use an instrumental haze test where optical limits are specified. |
| 4 | Moisture and Edge Durability | Quality PVB requires controlled moisture during storage and processing. Excess moisture can contribute to bubbles, whitening, or reduced edge durability after lamination. | Ionoplast materials generally provide higher moisture resistance than conventional PVB, but correct edge protection and processing remain necessary. | Review moisture-control records, perform accelerated humidity or boil-type testing when specified, and inspect laminated edges for bubbles, haze, and delamination. |
| 5 | Adhesion and Delamination Testing | The interlayer should maintain reliable adhesion to the selected glass under the specified environmental and impact conditions. | The interlayer should maintain adhesion and structural integrity under the design conditions, including environmental exposure where applicable. | Review test method, sample construction, conditioning, failure mode, and acceptance criteria. Results should reference applicable standards such as ISO 12543, EN 14449, or ASTM C1172 requirements. |
| 6 | Mechanical Performance | PVB provides impact retention and safety-glazing benefits, but its stiffness is strongly affected by temperature, loading duration, and formulation. | SGP generally has higher tensile stiffness and shear resistance than conventional PVB, making it suitable for applications requiring greater post-breakage stability when properly designed. | Check tensile, tear, shear, and load-deflection data at the design temperature and duration. Use structural calculations and project-specific testing rather than comparing one isolated strength value. |
| 7 | Impact and Safety Classification | The finished laminated glass should meet the required safety-glazing classification for the intended location and application. | The finished laminated glass should meet the required impact, breakage, and post-breakage criteria; the interlayer type alone does not establish compliance. | Verify complete-glass test reports against the applicable requirement, such as ANSI Z97.1, 16 CFR 1201, EN 12600, or the relevant local building code. |
| 8 | Certifications and Test Reports | Documents should identify the material grade, thickness, test construction, laboratory, test date, standard edition, and measured results. | Documents should clearly distinguish ionoplast performance from PVB performance and state the limits of the tested construction. | Confirm that reports are issued by a competent or accredited laboratory where required. Check whether the report covers the exact formulation, thickness, glass type, and production site supplied. |
| 9 | Packaging and Storage Condition | Packaging should protect the film from moisture, dust, ultraviolet exposure, puncture, and excessive heat. Storage conditions must follow the supplier’s instructions. | Packaging should prevent moisture ingress and mechanical damage. Even moisture-resistant ionoplast film must be kept clean, dry, and protected from contamination. | Inspect cartons, cores, seals, desiccant, pallet stability, and damage records. Record temperature, humidity, storage duration, and package-opening date. |
| 10 | Traceability and Batch Control | Each roll or package should be linked to a batch number, production date, material grade, nominal thickness, and quality-control record. | Each package should have a unique lot reference that can be connected to raw-material records, process data, inspection results, and shipment records. | Request a certificate of analysis and verify that the lot number on the roll, carton, invoice, test report, and delivery record is consistent and readable. |
Evaluation note: A valid comparison must use the same glass construction, interlayer thickness, conditioning method, test temperature, loading duration, and acceptance criteria. Product-specific technical data and applicable local regulations take precedence over generic comparison values.
Request the business license, registered address, export records, and manufacturing scope. The legal entity must match quotations, certificates, and bank documents. Do not trust websites alone.
Check the company through China’s official enterprise information system. Compare its registered address with the factory address. Small differences deserve clarification.
Not always. Inspect the certificate’s scope and issuing organization. A certificate covering trading activities may not prove manufacturing capacity.
Reports should identify glass thickness, interlayer type, dimensions, and testing standards. Confirm the report number directly with the laboratory. Check issue dates and product descriptions carefully.
Use neutral white light and a clean white background. Look for milky areas, bubbles, streaks, particles, wrinkles, and scratches. Packaging can hide defects.
Use a calibrated thickness gauge at several points. Record every reading, batch number, and measurement location. Uneven thickness may affect lamination and optical quality.
Request controlled peel tests, bending tests, impact tests, and aging data. Review results after heat and humidity exposure. Fresh samples are not enough.
Request batch numbers, production dates, interlayer thickness records, and storage conditions. Inspect edge sealing, moisture marks, clouding, and bubbles. A clean roll may still need testing.
An independent inspector can compare documents, samples, measurements, and factory conditions. Ask for photos and recorded results. My checklist has gaps.
This guide explains how to identify high-quality PVB vs SGP interlayers by examining their composition, structure, and performance requirements. It outlines how to verify a Chinese manufacturer’s credentials, technical documents, quality-control procedures, and product traceability before making a purchase. Readers will also learn how to inspect clarity, color consistency, thickness tolerance, surface cleanliness, and signs of contamination or handling damage.
The comparison focuses on practical differences in adhesion, mechanical strength, moisture resistance, safety performance, and suitability for various laminated-glass applications. It also recommends reviewing independent testing results, relevant certifications, packaging quality, batch information, and storage guidance. By combining visual inspection, document verification, sample testing, and supplier evaluation, buyers can make a more reliable judgment and reduce the risk of receiving inconsistent or unsuitable PVB or SGP interlayers.